Bildon Steel
Rust rarely begins as a dramatic failure. It often appears first beneath a washer, along a cut edge, or where water sits on a horizontal beam. In industrial facilities, these small areas can spread when moisture, salts, chemicals, and damaged coatings go unnoticed. The cost is not only cosmetic. Corrosion can shorten component life, interrupt operations, and complicate maintenance planning.
Understanding how to prevent rust in industrial steel structures starts with the conditions on site. A coastal plant, a washdown area, and a dry warehouse do not face the same exposure. Effective protection usually combines sound surface preparation, a coating system suited to the environment, thoughtful drainage, and regular inspection. Details matter: a blocked drain, a chipped coating near a weld, or a poorly protected bolt can become a recurring weak point. Rust starts quietly.
This guide covers practical ways to reduce corrosion risk, from selecting protective coatings to setting realistic inspection routines. It also considers design and maintenance choices that make steel easier to protect over time. Manufacturer guidance and qualified corrosion professionals should inform project-specific decisions, especially where aggressive exposure or critical structures are involved. No coating lasts forever. And a maintenance plan can still miss things; honest inspection notes and timely repairs help close that gap. The goal is not to promise rust-free steel, but to make deterioration visible, manageable, and less likely to disrupt the work that depends on it.
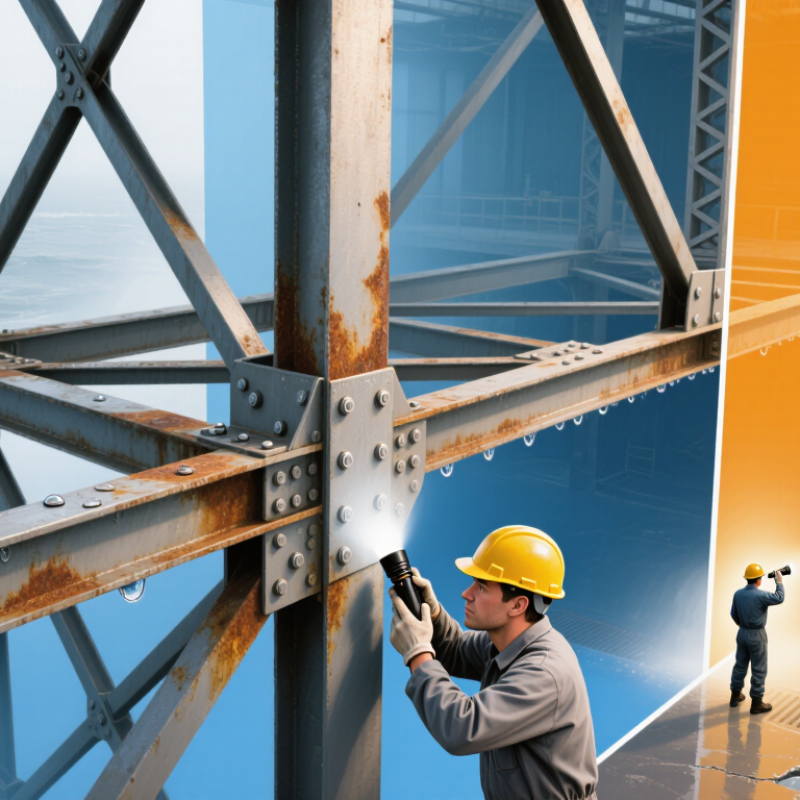
Rust begins when iron in steel meets oxygen and moisture. The process is electrochemical: small areas on the surface act differently, while a thin water film carries ions between them. Rain is not required. Overnight condensation can be enough, especially on cold beams or shaded connections. Salt, dust, and some industrial deposits make that film more conductive, speeding corrosion. It can happen quietly.
Damage often starts where protection is weakest. A scratch at a cut edge, a chipped coating near a bolt, or a narrow gap that traps water can expose bare steel. Crevices dry slowly. Dirt holds moisture. A leaking roof may keep one section damp while nearby steel stays dry, creating uneven corrosion.
The orange scale is a clue, not a full diagnosis. A small blister may hide deeper metal loss, while a surface stain may be shallow. That distinction is easy to miss from the ground. Inspection should note where moisture collects, whether coatings are lifting, and whether rust returns after cleaning. Site conditions vary, so appearance alone cannot reliably show how much steel remains.
Rust prevention starts with a site-specific risk assessment, not a standard coating choice. Record how often steel stays wet, where water collects, and how quickly surfaces dry. Look beneath beam seats, around bolt heads, inside hollow sections, and along weld toes. Small pockets matter. Salt spray, fertilizer dust, process fumes, and cleaning chemicals can accelerate corrosion, even indoors. Nearby coastlines are not the only concern; cooling towers and washdown areas create harsh local conditions. Temperature swings can also cause condensation on cold steel.
Map these conditions against the structure’s use and inspection history. Photographs after rain or washdown often reveal drainage failures that a dry-day inspection misses. Where failure could have serious consequences, combine visual checks with coating-thickness readings and ultrasonic steel-thickness measurements by trained inspectors. Compare results over time, since one measurement rarely tells the whole story. Watch for damaged edges, trapped debris, and coating blisters; each may point to a different cause. Risk scores can mislead. Exposure varies across a single frame, and access limits what inspectors can see. Document uncertain areas rather than assuming they are sound. This record helps maintenance teams target cleaning, drainage repairs, or coating renewal to actual site conditions.
Before applying any protective system, inspect the steel under bright, angled light. Look for mill scale, loose rust, oil, weld spatter, and sharp edges. A clean appearance is not proof of a ready surface. Small details matter. Grease around bolt holes can prevent proper coating adhesion, while salt near a coastal site may draw moisture beneath the coating. Remove oil with a suitable cleaner, then rinse and let the steel dry fully. Choose scraping or abrasive preparation to suit the steel condition and coating specification. Avoid polishing the surface smooth by accident; many systems need a defined anchor profile.
Pay extra attention to welds, corners, and the backs of stiffeners. These areas are easy to miss and often collect moisture. After preparation, remove dust with clean, dry air or a suitable vacuum. Check the profile and cleanliness against the coating specification. If soluble-salt testing is required, take readings at representative spots, not only the easiest ones. Apply protection within the specified time window, before flash rust or airborne dust returns. Record steel temperature, humidity, and dew point, and pause if condensation is likely. In the field, schedules can tempt crews to rush. That pressure deserves a second look; a small missed patch can become a costly repair.
| Preparation Step | Recommended Practice | How to Verify | Why It Helps Prevent Rust |
|---|---|---|---|
| 1. Remove oil and grease | Degrease contaminated areas with a suitable cleaning method before abrasive blasting or power-tool cleaning. Do not spread oily residue across the steel. | Inspect under good lighting and check for visible residue. Use the project-approved cleanliness test where required. | Oil and grease can interfere with coating adhesion and leave unprotected areas beneath the coating. |
| 2. Remove loose rust and mill scale | Choose preparation to match the coating specification and condition of the steel. Abrasive blasting to ISO 8501-1 Sa 2½ is commonly specified for high-performance protective coating systems; power-tool cleaning may suit less demanding or restricted areas. | Compare the prepared surface with the specified ISO 8501-1 visual reference grade. Record the method and inspection result. | Rust, loose scale, and weak material can undermine the coating and create early corrosion sites. |
| 3. Create the required surface profile | Select abrasive and blasting parameters to produce the profile required by the coating manufacturer. The appropriate profile varies by coating type and thickness. | Measure the anchor profile using an accepted method, such as a replica tape or profile gauge, and compare results with the project specification. | A suitable profile gives the coating an effective surface for mechanical adhesion without exceeding the coating’s ability to cover surface peaks. |
| 4. Remove soluble salts | Test for soluble contaminants when exposure history, marine conditions, or the project specification indicates a risk. Wash or otherwise clean the surface using an approved method if results exceed the specified limit. | Use a recognized field test, such as the ISO 8502-6 extraction method with conductivity measurement under ISO 8502-9. Apply the project-specific acceptance limit. | Salts left beneath a coating can attract moisture and contribute to osmotic blistering and underfilm corrosion. |
| 5. Control dust after cleaning | Remove abrasive residue and dust with clean, dry, oil-free compressed air or an approved vacuuming method. Avoid recontaminating prepared steel during handling. | Assess dust in accordance with ISO 8502-3 when specified, and document the required acceptance level. | Dust can weaken coating adhesion and create small pathways for moisture to reach the steel. |
| 6. Prepare edges, welds, and details | Remove weld spatter and sharp projections; smooth weld irregularities and prepare edges as required by the coating specification. Give crevices, corners, and attachments particular attention. | Visually inspect details before coating. Confirm that specified edge preparation and coating stripe coats are included in the work plan. | Coatings tend to be thinner or discontinuous at sharp edges and complex details, which can leave vulnerable spots. |
| 7. Check environmental conditions | Measure air temperature, steel temperature, relative humidity, and dew point before and during application. A commonly used control is to keep steel at least 3°C above the dew point, unless the product instructions or project specification require otherwise. | Use calibrated instruments and record readings at the work area. Follow the coating manufacturer’s limits for application and curing. | Condensation on steel can compromise adhesion and trap moisture beneath the protective coating. |
| 8. Coat promptly and inspect coverage | Apply the specified primer or coating as soon as practicable after preparation, before flash rust or new contamination develops. Apply the specified coats and stripe-coat details where required. | Check for visible contamination and flash rust before application. Measure dry-film thickness after curing using the method and limits in the project specification. | Prompt, complete coating reduces the time prepared steel is exposed to moisture and helps maintain a continuous barrier. |
Choosing a coating starts with the structure’s real exposure, not a generic product schedule. Note whether steel faces salt spray, chemical fumes, standing water, or repeated wet-and-dry cycles. A sheltered warehouse beam needs a different system from a pier column near the sea. Check operating temperatures and expected maintenance access, too.
Surface preparation matters just as much as coating selection. Remove oil, loose rust, and soluble salts using methods suitable for the site, then confirm the surface profile matches the coating specification. A zinc-rich primer, compatible intermediate coat, and durable topcoat can provide layered protection, but only when applied within the stated thickness and curing limits. Conditions vary. Record steel temperature, humidity, and dry-film thickness; these checks help explain early failures.
For complex structures, combine coatings with design measures such as drainage, sealed crevices, and electrical isolation between dissimilar metals. Pay special attention to welds, bolt heads, cut edges, and areas where water can collect. In practice, crews may miss small defects beneath clamps or around supports. Small defects matter. Plan close inspections after installation and repair damaged areas with compatible materials. Even a well-written specification can prove too optimistic when access is poor or site conditions change; revise the system when inspection evidence supports it.
2026 Top Ways to Prevent Rust in Industrial Steel Structures
Inspecting and Maintaining Rust Prevention Measures
A rust-prevention system is only reliable when inspections catch small failures early. The 2016 NACE IMPACT study estimated corrosion costs at US$2.5 trillion worldwide, or 3.4% of global GDP. It also estimated that better corrosion-control practices could save 15–35% of those costs. These figures are broad estimates, not a maintenance budget for any single facility. Still, they show why routine checks matter.
Walk the structure after heavy rain and look closely at welds, bolt heads, edges, and water-trapping joints. Blisters, chipped coating, orange staining, and rust creeping beneath paint deserve attention. Small defects matter. Record their locations with photos, dates, and readings from a calibrated dry-film-thickness gauge. Compare results with the project specification; a single universal inspection interval does not fit every exposure.
Remove loose rust and contamination before repairing damaged coating. Applying fresh paint over salt, dampness, or flaky material can hide the problem, not fix it. ISO 12944-7 gives guidance on coating application and supervision, but site conditions still shape the work. We sometimes focus too much on large, visible areas and miss the underside of a connection. That is an easy mistake to repeat. Keep repair records and revisit the same locations to check whether corrosion has returned.
Rust forms when iron meets oxygen and moisture. A thin water film can carry ions across the steel surface. Rain is not required. Overnight condensation may be enough.
It often starts at scratched edges, chipped coating near bolts, welds, or narrow gaps. Dirt and trapped water keep these areas damp. Small pockets matter.
Not reliably. A small coating blister may conceal deeper metal loss, while a stain may be shallow. A ground-level glance can fool us.
Salt, fertilizer dust, process fumes, and cleaning chemicals can make moisture more conductive. Cooling towers and washdown areas may create harsh conditions indoors, too. Exposure can vary across one frame.
Check beneath beam seats, around bolt heads, inside hollow sections, and along weld toes. Photos taken after rain or washdown can reveal poor drainage. Dry-day checks can miss it.
Where failure could have serious consequences, trained inspectors can combine visual checks with coating and ultrasonic steel-thickness readings. Compare results over time. One reading is not the whole story.
Look for loose rust, oil, mill scale, weld spatter, and sharp edges under angled light. Clean grease, remove dust, and let the steel dry fully. Clean-looking steel may still be unready.
Record steel temperature, humidity, and dew point. Pause if condensation is likely, and apply protection within the specified time window. Rushing can leave a missed patch. That deserves a second look.
Preventing rust in industrial steel structures starts with understanding how corrosion develops when steel is exposed to moisture, oxygen, salts, chemicals, or changing temperatures. Assessing the site’s environmental conditions and the structure’s use helps identify vulnerable areas and determine an appropriate level of protection. Before any protective treatment is applied, steel surfaces should be cleaned and prepared to remove rust, scale, oil, and other contaminants, allowing the chosen system to adhere effectively.
A practical approach to how to prevent rust in industrial steel structures combines suitable coatings or other corrosion-control measures with careful application and ongoing inspection. Protection should be selected for the structure’s exposure and maintained according to its condition. Regular checks can reveal scratches, coating failures, trapped moisture, or early corrosion before damage spreads. Prompt repairs and consistent maintenance help preserve structural performance, extend service life, and reduce the need for extensive restoration.